 AGCIS
Sintered parts manufacturing

Can I use sintering for my parts?
There are several limitations to consider when using sintering for metal parts:
- Size: We can supply parts ranging from Ø10 mm to Ø220 mm.
- Quantities: The MOQ for a sintering production batch is between 500 and 1,000 parts, depending on part size. Typical order quantities are closer to 10,000 parts.
- Part geometry: The process limits certain shapes; additional machining may be required, increasing the total cost.
- Material performance: Although sintered parts offer good strength, forging may be preferable for highly critical components.
Sintering references :
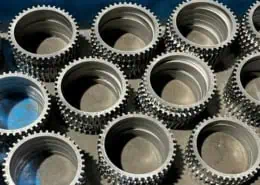
Why use sintering?
AGCIS outlines the key advantages of sintering below:
Suitable for certain complex geometries
For gears, sintering enables rapid production without additional machining. Axial holes can also be formed directly in the die.
High precision
Manufacturing tolerances differ for height and width. For width, standard tolerances are IT 8–9, equivalent to 0.08–0.09 mm for a 10 mm dimension. After sizing or calibration, tolerances of IT 5–7, equivalent to 0.05–0.07 mm for a 10 mm dimension, can be achieved.
For part height, tolerances are IT 10–13, equivalent to 0.10–0.13 mm for a 10 mm dimension.
High repeatability
The sintering process uses precision dies and high pressure, ensuring consistent part repeatability and stable quality.
Wide range of material options
Metal powders can be blended with a wide range of alloying elements, enabling an extensive range of material properties.
Lighter parts
Because sintered parts contain microscopic porosity, they can be lighter than equivalent cast or machined parts.
Surface roughness
Sintered parts generally have good surface roughness, which can be improved further through surface treatment at the end of the production process.
How does a sintering factory work?
The sintering process typically follows these stages:
First, the materials are blended to obtain a homogeneous mixture of metal powders.
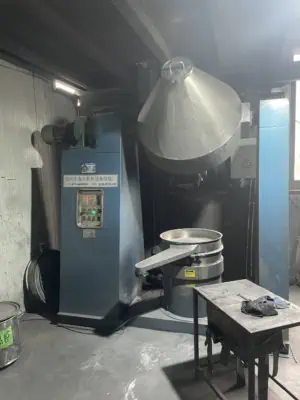
Metal powder blending
The powder is then compacted in a high-pressure moulding press.
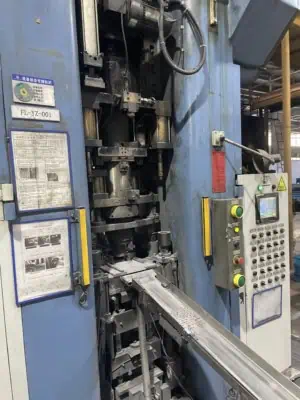
Sintering press
The compacted parts are then heated in a continuous oven to remove the lubricant.
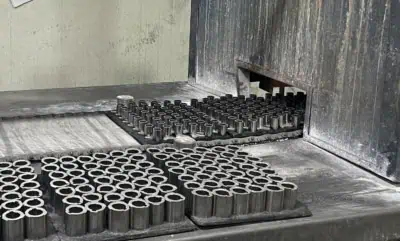
Lubricant removal by heating
The parts then enter a sintering furnace, where they are heated to just below their melting point.
Sintering furnace
If tight tolerances are required, the parts are pressed a second time in a calibration die.
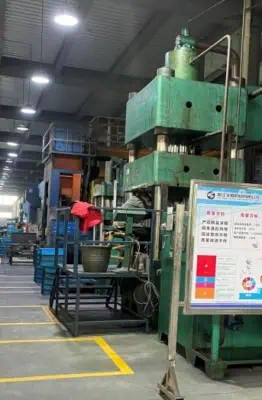
Calibration press
Finally, the parts are cooled and may receive additional post-processing, such as heat treatment, sanding or painting.