Plastics are everywhere, in your phone, car, and many other products. The most common solution is the plastic injection moulding, even if there are plenty of ways to make plastic parts, like 3D printing, thermoforming, or machining. What is a plastic injection factory, and how is it organized? It is what we will see in this article.
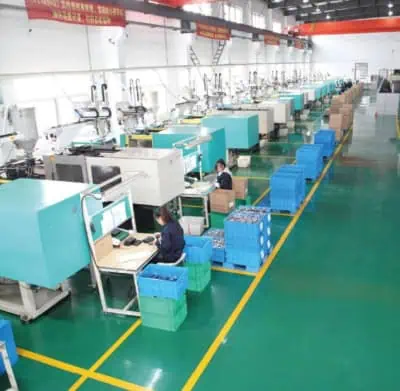
Plastic injection equipment
The plastic injection process is relatively simple to explain. Plastic, is heated at melting temperature and injected under pressure into a mold. The molten plastic cools and solidifies inside the mould cavity, forming the final shape of the part. Below are some details about this equipment that is the core of the plastic injection moulding factory.
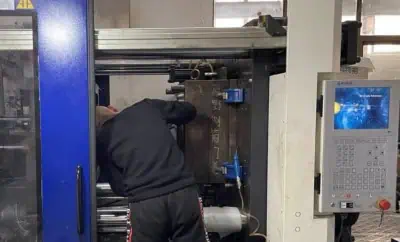
Injection molding machine
The process is called “Plastic injection moulding” because, like with a syringe, the melted plastic is pushed through the injection nozzles by injection screws. This step is done by a machine called injection press.
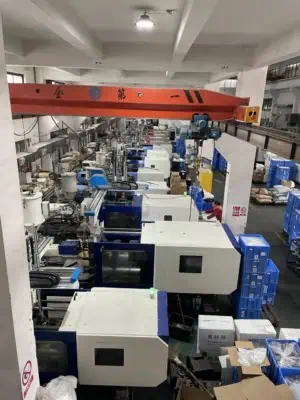
The injection press combines raw material heat, mold holding, and material under pressure. Presses are usually hydraulic but can also be electric.
These machines are set by clamping force that keeps the mould tightly closed. This strength range goes from a few dozen tons to several thousand tons.
Another critical setting in the press injection is the maximum injection pressure and maximum injection volume. These parameters define the maximum size of the parts injected in the press.
Injection moulds
Injection moulds are the critical element in manufacturing plastic parts. The molten plastic is injected under pressure into the mould cavity, where it cools and solidifies to form the part. The mold is made of two mould halves attached to the injection press. One mould half is fix while the other one is moving. The moving half mould is to let the mould open for parts release.
According to the part’s complexity, moulds can be simple or complex matrices with drawers (activated by jacks).
To guarantee a suitable plastic cooling down and prevent shrinkage, this is recommended to add hot runners and a cooling-down system through the mould with a cooling-down liquid.
Injection moulds are generally made of steel (sometimes aluminum for Small quantities – plastic injection). They can have several cavities to create several parts at each injection.
Mould design and manufacturing are such a specialty. It has to consider clearance angles and ejectors locations to make a good mould release, as well as the parting line located at the meeting of the two mould parts. With proper maintenance, the mould can be used for a large number of injection cycles, depending on its material and design.
Additional equipment
In addition to the primary equipment for plastic injection, factories can also use other equipment.
Additional equipment can be robots and conveyors for the parts release, marking equipment, or ultrasonic welding tools for assembly.
A dedicated quality control area is generally set up for plastic injection.
Plastic injection raw material.
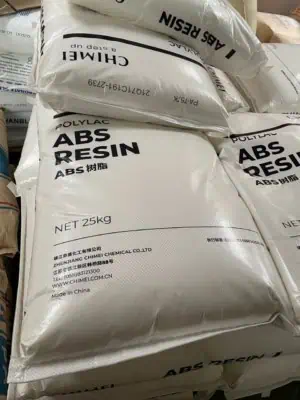
The plastic injection factory also has to plan raw materials sourcing. The raw material looks like small pellets and is delivered and stored in big bags. The material can be affected by intense humidity and should be kept under good packaging conditions to prevent this. An additional drying operation before injection may be needed for hygroscopic materials like PA, PC or PEEK.
The plastic pellets can be colored or not. Mixing colored and neutral pellets to get a good final product color is a common practice.
Raw plastic suppliers are numerous (COVESTRO, Chimei, SABIC, etc..), as well as the kinds of plastics (ABS, PC, PE, PEEK, POM, PA, etc.) and the grades (anti UV, flame-retardant, optical, etc.). Factories should anticipate clients’ specific requirements by making their stock with various materials and sources.
Plastic injection factory labor
Assuming that it is automated and assisted by robots, running a plastic injection press doesn’t need many people, and only one operator can supervise several injection machines. On the other hand, machines settings and mold adjustments need some operating time.
However, some parts need an over-molding, either on inserts or a metallic structure, that must be manually set up before each injection.
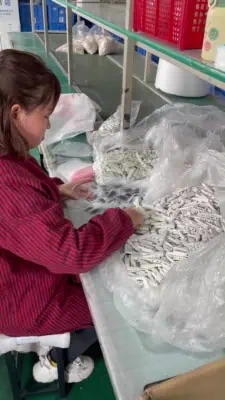
Furthermore, part finishing after injection can require much more operators. Part deburring is often manually done, and screen printing marking also needs an operator.
Eventually, the factory can also run the parts assembly and the packaging if the labor cost is low. That is common in low-cost labor countries like China.